Building Better Supplement Formulations Through Careful Ingredient Selection

Modern supplement development combines nutrition science, manufacturing technology, quality control, and product design. As manufacturers explore more sophisticated ingredient formats, the process of selecting and incorporating raw materials becomes increasingly important.
Specialized delivery systems can introduce additional technical considerations. For formulators, understanding the characteristics of a raw material before commercial production can help create a smoother path from laboratory development to manufacturing.
Read Also: How Your Meal Preparation Speed Influences Digestive Enzyme Production
Start With Formulation Requirements
Every product begins with a concept. Before selecting individual ingredients, developers should establish the product’s intended format and manufacturing requirements.
A capsule may require a different powder profile from a drink mix. Similarly, a liquid product may have different stability and dispersion requirements than a dry powder.
Clearly defining these factors gives the R&D team a framework for evaluating potential ingredients.
Review Ingredient Characteristics
Raw materials can differ considerably even when they belong to the same general ingredient category.
Formulators should review factors such as:
- Physical appearance
- Powder flow
- Particle size
- Moisture content
- Concentration
- Dispersion
- Storage conditions
- Stability
- Compatibility
These characteristics can influence both formulation performance and production efficiency.
The Role of Specialized Delivery Formats
Liposomal delivery systems are based on lipid structures that can be used to formulate certain compounds. Their characteristics depend on the specific formulation and manufacturing process.
This means manufacturers should evaluate each material individually rather than assuming all products using the same delivery terminology will perform identically.
Technical specifications and supplier documentation can provide a starting point for comparison.
Compatibility Is Essential
A raw material rarely works alone. Most commercial formulations contain several ingredients that need to remain compatible throughout processing and storage.
Compatibility testing can identify interactions that may affect physical appearance, dispersion, taste, stability, or other product characteristics.
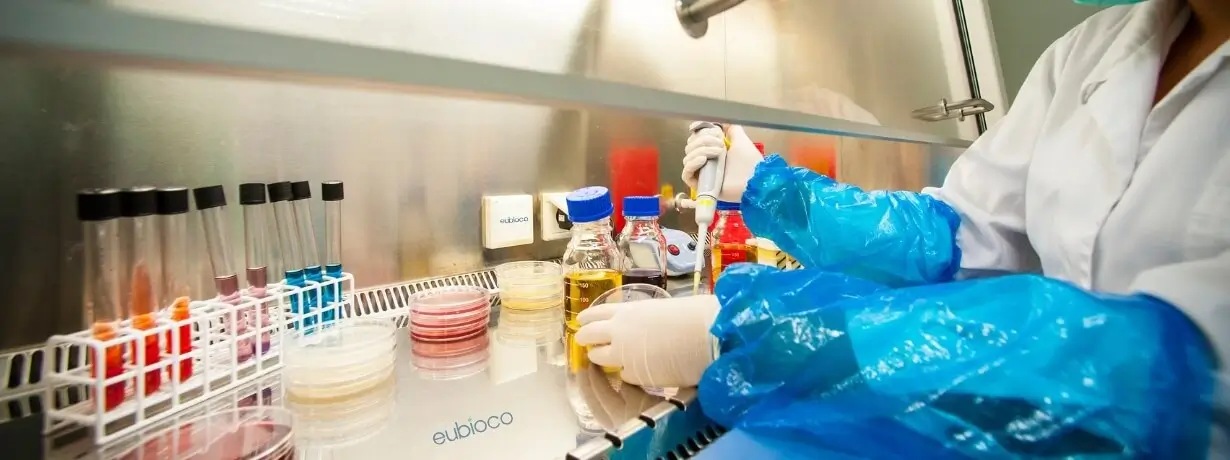
Developers can conduct laboratory trials using different concentrations and combinations to identify a suitable formulation.
Stability Testing
Stability testing helps determine how a formulation behaves over time under defined conditions.
Depending on the product, development teams may examine changes in appearance, moisture, dispersion, chemical characteristics, packaging condition, or other relevant parameters.
Testing should reflect the intended storage environment and packaging configuration as closely as possible.
Selecting a Reliable Raw-Material Partner
A supplier can influence the efficiency of the entire development process. Reliable documentation, consistent batches, clear communication, and appropriate packaging can reduce unnecessary complications.
Manufacturers should also consider whether the supplier can support future production volumes.
For companies evaluating ingredients for new supplement concepts, EmerWell Liposomal Curcumin Powder offers an example of a specialized powder ingredient that can be assessed based on formulation specifications and application requirements.
Managing Scale-Up
A formulation that works in a laboratory may behave differently during commercial production.
Scale-up changes can affect mixing time, equipment geometry, temperature exposure, material flow, and other processing conditions.
Pilot-scale trials provide an opportunity to identify these differences. Development teams can then adjust the manufacturing process before moving to full-scale production.
Maintain Strong Quality Controls
Quality control should be integrated throughout the product lifecycle.
Incoming raw materials should be checked against approved specifications. Production batches should be monitored according to established procedures, and finished products should undergo appropriate testing.
Batch records and traceability systems can also make it easier to investigate deviations or supplier-related changes.
Plan for Long-Term Supply
Commercial success requires more than an effective laboratory formulation. Manufacturers need a stable supply of raw materials.
Before launch, purchasing teams should consider supplier capacity, minimum order quantities, lead times, packaging sizes, shipping conditions, and potential supply risks.
Maintaining qualified alternative suppliers may also provide additional flexibility, although any replacement material should undergo appropriate evaluation before use.
Continuous Product Improvement
Formulation work can continue after launch. Manufacturers may identify opportunities to improve processing efficiency, packaging, sensory characteristics, stability, or cost.
Supplier feedback and production data can help identify areas where adjustments may be useful.
A continuous-improvement approach allows companies to respond to manufacturing observations while maintaining established quality requirements.
FAQs
What makes ingredient selection important in supplement development?
Ingredient characteristics influence formulation, processing, stability, quality, packaging, and overall manufacturing performance. Selecting materials that fit the intended product can simplify development.
Why are pilot trials important?
Pilot trials help manufacturers understand how a formulation behaves at a larger scale and identify processing differences before full commercial production.
How should manufacturers evaluate specialized ingredient suppliers?
They can review technical documentation, quality systems, batch consistency, sample support, storage and packaging information, production capacity, lead times, and technical communication.
Conclusion
Careful ingredient selection provides an important foundation for successful supplement development. Specialized delivery formats can offer additional formulation possibilities, but each raw material should be evaluated according to its specific characteristics and intended application. By combining laboratory testing, stability assessment, supplier qualification, scale-up planning, and strong quality controls, manufacturers can create a more reliable path from initial formulation concept to commercial production.